

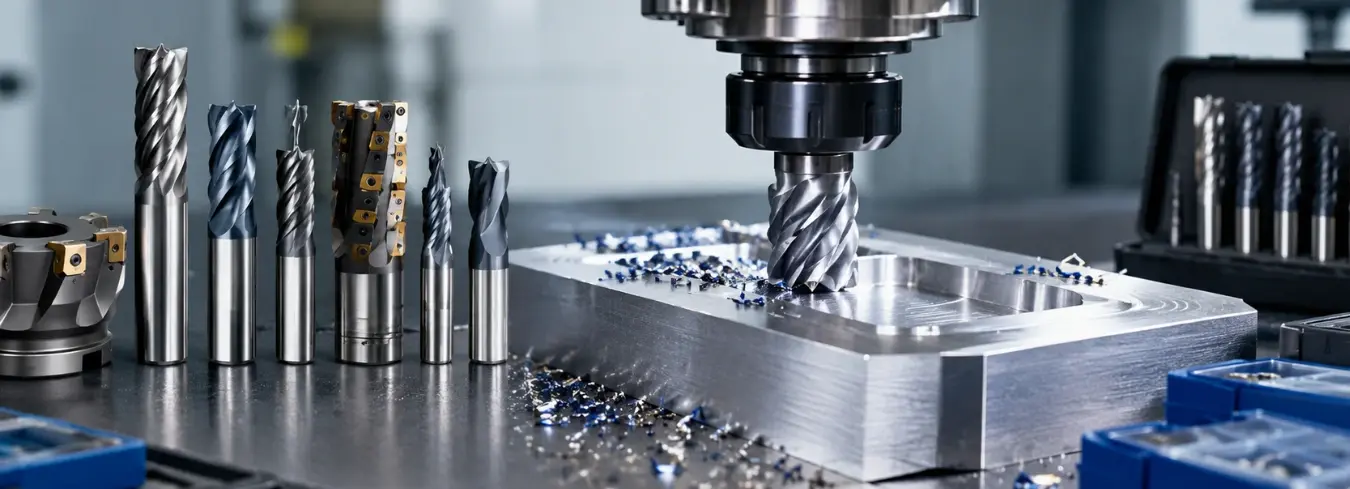
A milling cutter is a rotary cutting tool used in milling machines and CNC machining centres to remove material from a workpiece. It spins at high speed while the workpiece feeds into it, cutting away metal, plastic, or composite material to create flat surfaces, slots, pockets, contours, and complex 3D shapes.
Get the right milling cutter for the job, and you get clean cuts, long tool life, and accurate parts. Get it wrong, and you get broken tools, poor surface finish, and scrapped components.
This guide covers every milling cutter type, how to select the right one, and the best practices that keep your tools cutting efficiently in UAE workshops, fabrication facilities, and CNC machining environments.
Types of Milling Cutters: What Each One Does
End Mill Cutters
The end mill is the most used milling cutter in any workshop. It cuts on the end and on the sides, which means it can plunge into material, cut slots, machine profiles, and produce pockets – all with one tool.
End mills come in several geometries:
- Flat end mill (square end mill) has a sharp 90-degree corner at the tip. Used for slotting, profiling, facing, and pocketing where square corners are required. The most common end mill in general workshop use.
- Ball nose end mill has a hemispherical tip. Used for 3D contouring, curved surfaces, and mould work. The round nose produces smooth transitions across contoured surfaces without leaving sharp step marks.
- Corner radius end mill has a small radius at the corner instead of a sharp edge. The radius spreads cutting forces across a wider area, which reduces tool wear and extends life compared to a sharp corner end mill. A practical choice for general production milling where tool life matters.
- Roughing end mill (rippa cutter) has a serrated cutting edge along the flutes. This geometry breaks chips into smaller pieces, which reduces cutting forces and allows high material removal rates. Used for rough machining to remove large amounts of stock quickly before a finish cut.
Face Mill Cutters
A face mill has cutting inserts arranged around its circumference and face. It cuts on the bottom and produces flat, smooth surfaces across wide areas in a single pass. Face mills are indexable – the inserts are replaced when worn rather than replacing the whole cutter body. This makes them more economical for high-volume facing operations.
Used in: surface facing, producing flat reference surfaces, removing scale from castings.
Ball Nose Cutters
Already listed under end mills, but worth a separate note. Ball nose cutters are the standard tool for 3-axis and 5-axis CNC profiling work – mould cavities, aerospace components, and any part with curved geometry. The smaller the stepover used, the smoother the surface finish.
Slot Drill Cutters
A slot drill looks similar to an end mill but is designed specifically for plunging into material and cutting slots. Most slot drills have two flutes and a centre-cutting geometry that allows direct plunge entry without pre-drilling. Used for keyways, slots, and any application requiring a cutter to start from a solid surface.
T-Slot Cutters
A T-slot cutter has a disc-shaped cutting head on a narrow neck. It enters an existing slot and cuts sideways to create the T-shaped profile. Used for machine table T-slots, fixture rails, and components that require T-slot fixturing systems.
Dovetail Cutters
Similar in principle to T-slot cutters but the cutting head is angled to produce a dovetail profile. Used for dovetail slides, fixture grooves, and precision locking features.
Thread Mill Cutters
A thread mill cuts helical thread paths in CNC machining centres. Unlike a tap, a thread mill can cut multiple thread sizes and both left and right-hand threads with the same tool by adjusting the helix path. Used for large-diameter threads, blind hole threads, and materials where tap breakage risk is high.
Shell Mill Cutters
A shell mill is a large-diameter face mill that mounts on an arbor. Used for high-volume facing of large flat surfaces where a standard face mill is too small. Common in heavy manufacturing, structural fabrication, and mould base preparation.
Slitting Saw Cutters
A thin disc cutter mounted on an arbor. Used for parting off, cutting slots, and cutting material to length on a milling machine. The thin profile removes minimal material and produces precise, narrow cuts.
Milling Cutter Materials: HSS vs Carbide
The material the cutter is made from determines how fast it cuts, how long it lasts, and which workpiece materials it can handle.
Cutter Material | Best For | Cutting Speed | Tool Life | Cost |
HSS (High-Speed Steel) | Mild steel, aluminium, general workshop use | Moderate | Good | Low |
HSS-Co (Cobalt HSS) | Stainless steel, alloy steel, tougher materials | Moderate to high | Better than HSS | Medium |
Solid Carbide | All metals, high-speed CNC, hard materials | High | Excellent | Higher |
Indexable Carbide Inserts | High-volume production, facing, heavy cutting | High | Replace inserts only | Most economical at volume |
Carbide inserts are the standard for production CNC milling in UAE manufacturing and fabrication facilities. Solid carbide end mills deliver the best performance for small-diameter, high-precision work. HSS tools remain practical for manual milling and lower-volume workshop jobs.
Coatings extend carbide tool life further:
- TiN (Titanium Nitride) – general purpose, gold coloured, reduces friction
- TiCN – harder than TiN, better wear resistance
- TiAlN – excellent heat resistance, suited to dry cutting and high-speed machining
- AlTiN – for the most demanding high-temperature cutting environments
How to Select the Right Milling Cutter
Selection comes down to five factors. Work through each one before choosing a tool.
1. What Material Are You Cutting?
Material determines grade, geometry, and coating.
Material | Recommended Cutter | Key Consideration |
Mild steel | HSS or carbide, standard geometry | Most forgiving material |
Stainless steel | Carbide, TiAlN coated, sharp edge geometry | Work-hardens – keep tool sharp and feeds consistent |
Aluminium | Sharp carbide, polished flutes, high rake angle | Needs chip clearance – use 2 or 3 flute end mills |
Cast iron | Carbide, robust geometry | Abrasive – coated tools extend life |
Hardened steel | Solid carbide, ball nose, small stepover | Low cutting speeds, rigid setup essential |
Titanium | Carbide, TiAlN coated, climb milling | Generates high heat – coolant critical |
2. What Operation Are You Performing?
- Facing a flat surface: face mill or shell mill
- Slotting: slot drill or end mill
- Profiling: end mill
- 3D contouring: ball nose end mill
- Rough material removal: roughing end mill or indexable face mill
- Finishing to a smooth surface: fine-pitch end mill or ball nose with small stepover
- Thread cutting: thread mill or tap
3. How Many Flutes Do You Need?
Flute count affects chip clearance and surface finish.
- 2 flutes – more chip clearance, suited to aluminium and soft materials
- 3 flutes – balance of chip clearance and finish, general purpose
- 4 flutes – better surface finish, suited to steel and harder materials
- 5 or more flutes – finishing operations, hard materials, high-speed machining
More flutes produce a better finish. Fewer flutes clear chips more effectively. Aluminium always needs fewer flutes – packed chips in aluminium break tools.
4. What Is Your Machine Capable Of?
A milling cutter that suits the job must also suit the machine running it.
Check these before selecting a cutter:
- Spindle speed (RPM) – does the machine reach the cutting speed the tool requires?
- Spindle power – can it maintain that speed under cutting load?
- Rigidity – a lighter machine cannot run aggressive cuts without vibration
- Toolholding – does the shank size and type match your collet or chuck?
- Coolant – through-spindle coolant changes which coatings and cuts are practical
Running a carbide end mill at half its rated cutting speed because the machine cannot reach the required RPM wastes the tool’s capability and produces a worse result than a properly matched HSS cutter would at the correct speed.
5. What Surface Finish Is Required?
Roughing operations remove stock fast with less attention to finish. Finishing operations use lighter cuts, sharper tools, and higher speeds to hit the required surface quality.
For rough machining: use a roughing end mill or large face mill, high feed rates, full depth of cut, and accept a rougher surface.
For finishing: reduce depth of cut, increase spindle speed, use a sharp fine-tooth cutter, and slow the feed rate. Ball nose cutters with small stepover values produce the best contoured surface finish.
Milling Best Practices: What Separates Good Results from Bad Ones
Use Climb Milling for Better Finish
There are two ways to feed a workpiece into a milling cutter. Conventional milling feeds against the cutter rotation. Climb milling feeds with it.
Climb milling produces a better surface finish, reduces cutting forces on the workpiece, and extends tool life. Use climb milling for finishing cuts on rigid machines. Use conventional milling for roughing on less rigid setups or when machining scale-covered castings, where the initial cut can damage a climb milling entry.
Set Cutting Speed Correctly
Every milling cutter has a recommended surface cutting speed (Vc) for the material being cut. Running too slow wastes time. Running too fast burns the tool.
The formula: RPM = (Vc x 1000) / (pi x cutter diameter)
Most cutter manufacturers publish recommended cutting speeds for each material and coating. Start within those values. Adjust from there based on actual chip formation and tool temperature.
Manage Chips and Coolant
Chips that stay in the cutting zone get re-cut. Re-cut chips damage the surface finish and the cutter. Good chip clearance is as important as the cut itself.
For aluminium: use plenty of coolant or air blast to clear chips. Aluminium chips pack into flutes and break tools.
For steel: flood coolant at the cutting zone, not from above. The coolant needs to reach the tip.
For dry cutting with coated carbide: air blast clears chips without the thermal shock of intermittent coolant.
Match Depth of Cut to Tool Diameter
A general starting point: axial depth of cut (cutting depth along the tool axis) of 1 to 1.5 times the cutter diameter for roughing. Radial depth of cut (how much of the cutter width is engaged) of 50 percent for slotting, 25 to 30 percent for side milling.
These are starting points. Harder materials, less rigid machines, and longer tool overhangs all require more conservative cuts.
Control Tool Overhang
The longer the tool sticks out from the holder, the more it deflects under cutting force. Deflection causes vibration, poor surface finish, and premature tool breakage.
Use the shortest tool length that clears the workpiece. If deep features require long reach, reduce cutting depth and feed rate to compensate.
Check Tool Runout Before Cutting
Runout is how much the tool tip wobbles off-centre as it spins. Even 0.02 mm of runout causes uneven chip loads across the flutes, which accelerates wear and reduces surface finish quality.
Check runout with a dial test indicator before each setup. Measuring instruments including dial test indicators and digital indicators are essential workshop tools for any facility running milling operations.
Use the Right Toolholding
Tool holders affect rigidity, runout, and balance. Collet chucks (ER collets) are the most common. Hydraulic chucks and shrink-fit holders offer better rigidity and lower runout for high-speed and precision applications.
Never use a worn or damaged collet. A collet that does not hold the shank concentrically defeats any accuracy the cutter is capable of delivering.
CNC Milling vs Manual Milling: Different Priorities, Same Principles
The selection and best practice principles above apply to both CNC and manual milling. The difference is in how the parameters are controlled.
On a CNC machine, cutting speed, feed rate, depth of cut, and toolpath are set in the programme. Consistency is built in. The operator sets up the machine, proves out the programme, and monitors the cut.
On a manual milling machine, the operator controls feed rate by hand, which introduces more variation. This makes tool selection even more critical on manual machines – a cutter that is more forgiving of variation in feed and speed performs better in manual operations than one that requires precise parameter control to perform correctly.
Common Milling Cutter Mistakes to Avoid
- Running the wrong speed for the material. Too fast burns carbide. Too slow on aluminium causes built-up edge on the tool, where workpiece material welds to the cutting edge and ruins finish and accuracy.
- Using too many flutes on aluminium. Four-flute end mills pack with aluminium chips. Use two or three flutes and clear chips aggressively.
- Excessive tool overhang. Every extra millimetre of overhang reduces rigidity. Use the shortest tool that clears the part.
- Ignoring tool runout. A tool running with 0.05 mm runout is effectively cutting with one flute doing most of the work. Check runout before every setup.
- Using the same tool for roughing and finishing. A roughing tool that has removed significant stock is no longer sharp enough for a quality finish. Use separate tools – rough with one, finish with another.
- Wrong cutter for the material. A standard HSS end mill on stainless steel work-hardens the surface and dulls within minutes. Match the grade and coating to the material every time.
Quick Selection Reference
Job | Cutter Type | Material Grade | Flutes |
Flat surface facing | Face mill or shell mill | Indexable carbide | N/A (insert dependent) |
Slotting | Slot drill or end mill | Carbide or HSS | 2 to 3 |
Profiling steel | Flat end mill | Carbide, TiAlN coated | 4 |
Profiling aluminium | Flat end mill | Carbide, polished | 2 to 3 |
3D contouring | Ball nose end mill | Solid carbide | 2 to 4 |
Rough stock removal | Roughing end mill | Carbide or HSS-Co | 4 to 6 |
T-slot cutting | T-slot cutter | HSS or carbide | N/A |
Thread cutting (CNC) | Thread mill | Solid carbide | N/A |
Parting and slitting | Slitting saw | HSS or carbide | N/A |
Conclusion
The cutter is not the problem. It is almost never the cutter. Wrong material grade. Wrong speed. Too much overhang. Wrong number of flutes for aluminium. These are the real reasons tools fail and parts get scrapped. The cutter just takes the blame. Pick the right tool for the right job, set it up correctly, and run it at the right speed. That is the whole game.
For quality CNC machine tools, milling cutters, and carbide inserts in UAE, visit arhtrd.com, a trusted industrial tools supplier in Dubai.
What is the difference between an end mill and a milling cutter?
All end mills are milling cutters, but not all milling cutters are end mills. Milling cutter is the broad term covering face mills, slot drills, ball nose cutters, T-slot cutters, and many others. End mills are a specific type within that category, designed for profiling, slotting, and pocketing.
Can I use a milling cutter on a lathe?
Live tooling on CNC lathes allows milling cutters to be used for off-centre features, slots, and cross-holes on turned components. On a standard lathe machine, milling cutters are not used – that is a milling machine operation.
What is the best milling cutter for stainless steel?
Solid carbide end mills with TiAlN coating and a sharp geometry designed for stainless. Stainless work-hardens quickly, so the cutter must stay sharp, feeds must remain consistent, and dwell in the cut must be avoided.
How do I know when a milling cutter is worn?
Signs of wear include increased cutting noise and vibration, deteriorating surface finish, blue or brown discolouration on the tool tip (heat sign), and visible flank wear on the cutting edges under a loupe or inspection lens.
What does climb milling mean?
Climb milling feeds the workpiece in the same direction as the cutter rotation. It produces better surface finish, reduces cutting forces on the part, and extends tool life compared to conventional milling, where the feed is opposite to cutter rotation. Use climb milling for finishing cuts on rigid machines.
How often should milling cutters be replaced?
There is no fixed interval. Replace when surface finish degrades, when cutting forces increase noticeably, or when visible wear appears on the cutting edges. Inspect tools regularly, especially after machining hard or abrasive materials.